Alright, let’s cut to the chase—if you’re running a facility that relies on hot oil boilers (HOBs), you already know these bad boys are workhorses for everything from food processing to chemical manufacturing. They transfer heat efficiently without turning water to steam, which makes them way more versatile than steam systems for high-temp, low-pressure needs. But here’s the thing: skip the safety precautions, and a "workhorse" can turn into a nightmare real fast. I’m a hot oil boiler supplier, and I’ve seen enough close calls (and a few full-on messes) to know that most issues aren’t because the boiler is garbage—they’re because operators skipped the small, obvious steps. Let’s break down what actually works, no stuffy jargon or generic rules you’ll forget. Hot Oil Boiler
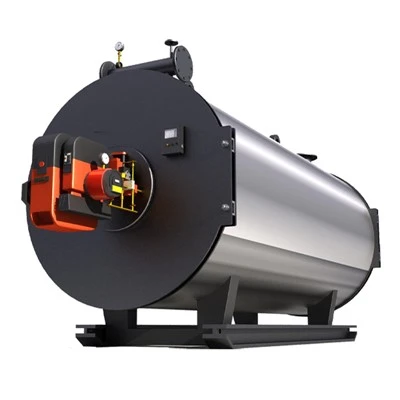
First off, let’s get one thing straight: hot oil isn’t like water. It doesn’t boil at 212°F; it can hit 500°F and still be liquid, but that also means it’s way more flammable if it leaks. I had a customer last year who forgot to replace a tiny seal on a pipeline—$12k in floor repairs, three days of downtime, and a near-miss when the oil hit a nearby hot surface. That’s why pre-start checks aren’t just box-ticking exercises; they’re your first line of defense.
Before you even fire up the boiler after a shutdown (even a weekend one), don’t just hit the power button. Let’s start with the oil itself. First, check its thermal stability. Over time, hot oil breaks down—contaminants build up, viscosity gets all weird, and the flash point drops. If the flash point is lower than the manufacturer’s recommendation (usually around 100°F below operating temp), that’s a red flag. Last quarter, a textile plant I supply had oil that was 80°F under the flash point limit—they didn’t catch it, and when the boiler cycled, the oil ignited in the expansion tank. Totaled the tank, took their whole line down for a week. Not fun. Also, check the oil level in the expansion tank—too low, and you’ll get air in the system (air = oxidation = more breakdown); too high, and when the oil heats up and expands, it’ll overflow. Easy fix: keep the level 1/3 to 1/2 full at all times, no exceptions.
Next, leak checks. This isn’t a quick once-over with a flashlight. I tell every new client to do a pressure test first—charge the system with dry nitrogen (not compressed air, which has moisture) to 10-15 psi above operating pressure, then shut off the gas and watch the gauge. If it drops more than 2 psi in an hour, you’ve got a leak. And don’t just look at the obvious joints—check pipe hangers, valve stems, pump seals, and especially the expansion tank’s vent line. Small leaks are the worst because they dry out, leaving a gummy residue that hides bigger leaks until it’s too late.
Once you’ve done pre-start, you can fire it up—but don’t crank the temp to max right away. Gradual heating is non-negotiable. Here’s why: steel expands when it gets hot, and if you heat the boiler too fast, you’ll cause thermal stress, which cracks pipes or welds. I recommend ramping the temp no more than 50°F per hour until you hit 200°F, then holding that for an hour to let all the moisture in the oil and system evaporate (moisture mixed with hot oil causes foaming, which leads to overheating and burnout). Then ramp again to your operating temp, same 50°F per hour, hold for two hours to let everything settle. Skipping this gradual ramp? I’ve seen a boiler’s heat exchanger crack so bad they had to replace the whole unit, and that’s a $20k+ bill for no reason.
Now, the day-to-day stuff. Operators can’t just check a gauge once a shift and call it good. Let’s talk about the big three: temperature, pressure, and flow rate. First, the outlet oil temp—never let it exceed the manufacturer’s set point. Most HOBs have a high-limit switch that shuts the burner off if it gets too hot, but don’t rely solely on that. I’ve seen instances where a bad sensor made the switch not trigger, so the oil hit 600°F and coked (turned to solid carbon) on the heat exchanger, blocking flow. That leads to overheating the metal, warping it, and that’s a catastrophic failure. So check the temp gauge every hour, not every four.
Pressure is another one. The system pressure should stay steady when operating, not spike or drop. A pressure spike usually means flow is blocked (coked oil, a closed valve, or a faulty pump), which leads to overheating. A pressure drop? Almost always a leak, which we already talked about, but can also be a bad pump. Last month, a food manufacturer called me in because their pressure was dropping every hour—turned out the pump seal was failing, and they were losing oil into the pump housing. We replaced the seal for $800, but if they’d waited a week, the pump would’ve seized, and they’d be down for 3 days.
Flow rate is the most overlooked one. If the oil isn’t circulating fast enough through the heat exchanger, it’ll sit there and get too hot, coking and eventually burning. How do you check it? Most systems have a flow meter, but if yours doesn’t, just listen to the pump—normal operation is a steady hum; if it’s making a high-pitched whine, that’s cavitation, which means low flow. Also, check the return oil temp—if it’s way lower than the outlet temp, that means the oil isn’t moving through the system like it should. I can’t stress this enough: if flow drops, shut the burner off immediately, don’t wait.
Then there’s maintenance, which is the boring part but saves you from 99% of issues. Let’s start with the pump. It’s the heart of the system, right? Change the pump’s oil seal every 6 months if you run 24/7, 12 months if it’s on a weekend schedule. Check the pump’s bearing grease monthly—overgrease and you’ll burn the bearing; undergrease and it seizes. I had a brewery client who only greased the pump once a year, and a bearing locked up, causing the pump to snap a shaft—they had to shut down their brew line for 5 days, losing $50k in product. Ouch.
Next, the heat exchanger. You need to clean it every 1-2 years, even if the oil looks fine. Coking builds up on the inside over time, insulating the heat transfer, which makes the boiler work harder, raises temps, and increases fire risk. How do you clean it? Usually a chemical flush, but don’t use harsh chemicals without checking with the oil supplier—some chemicals will react with the hot oil and cause foaming. I always tell clients to do a sample test first: mix a small amount of chemical with used oil, if it foams more than 10 seconds, skip it.
And don’t forget the safety devices. The high-limit temp switch, pressure relief valves, flame sensors—these are not install-it-and-forget-it. Test the pressure relief valve every 3 months: manually open it (following the manufacturer’s steps, don’t just yank it) to make sure it’s not stuck, then close it. If it doesn’t hold pressure after testing, replace it immediately. Last year, a printing plant’s relief valve was stuck shut, and when the system overpressurized, the pipe fittings blew—sprayed hot oil all over their electric panel, caused a small fire that took out their whole facility’s power. The fire department said if the relief valve had worked, it would’ve been a 10-minute fix, not a total loss. Flame sensors? Clean them every 6 months—they get covered in soot, so they can’t detect if the burner is lit, leading to unburned gas building up and an explosion if the burner reignites.
Now, what about operator training? This is the #1 thing that most suppliers (not me, I promise) skip when they sell you a boiler. If your operator doesn’t know how to read the gauges, what’s a normal temp vs. an emergency temp, or what to do if the flow drops, all the safety devices in the world won’t help. I always include a 2-day training session with every HOB I sell—we go through pre-start, daily checks, emergency shutdown, and common issues. Last month, a new client told me their old supplier only did a 30-minute walkthrough, and their operator accidentally closed a valve, caused overheating, and ruined $15k worth of oil. That’s preventable. Also, make sure operators know the emergency shutdown (ESD) procedure: where the ESD button is, what to shut off first (burner, then fuel supply), and who to call. Post the ESD steps right by the boiler, taped to the wall—don’t make them remember it.
Wait, let’s talk about something I see all the time: modifications. Don’t change the boiler or the system without consulting your supplier or a certified tech. I had a client who wanted to add a new piece of equipment to the hot oil loop, so they cranked the pump to push more oil, which made the pressure spike, the relief valve open, and oil spilled all over the floor. The pump wasn’t rated for that higher flow, and they didn’t check with anyone. Always run any changes by the supplier—we’ll tell you if the system can handle it, or what you need to adjust.
Also, fire safety. Even with all these checks, hot oil is flammable, so don’t take chances. Keep a Class B fire extinguisher (for flammable liquids) within 10 feet of the boiler, not down the hall. No rags, paper, or other combustibles within 20 feet. Have a spill kit on hand—absorbent pads, not just water. If there’s a hot oil spill, don’t use water—hot oil will float on water and spread the fire. Let it cool, then use the absorbent pads.
Now, let’s cover common myths that get people in trouble. Myth 1: “Hot oil doesn’t need maintenance like water boilers.” No, actually, hot oil degrades faster than water, and leaks are way harder to catch. Myth 2: “I can run the boiler 10°F over the set point to save time.” That’s a fast track to coked oil and a failed heat exchanger. Myth 3: “I don’t need to replace oil until it looks dirty.” No—oil can be dirty on the outside but have a dropped flash point on the inside, which is invisible until it ignites.
At the end of the day, safety for hot oil boilers isn’t about following a 50-page manual you’ll never read—it’s about consistent, small steps every day. Check the flow, check the pressure, check the oil level, test the valves, and train your people. I’ve been supplying HOBs for 12 years, and the most successful clients are the ones that stick to these basics, not the ones that buy the most expensive equipment or skip steps to save time.

If you’re dealing with a hot oil boiler, whether you’re having issues, need a new one, or just want to go over safety checks, hit me up for a no-pressure chat. I don’t do sales pitches that sound like a robot—we’ll talk about your specific setup, common issues in your industry, and make sure you’re not leaving gaps that could turn into a disaster. Let’s keep your facility running, not shutting down.
Condensing Steam Boiler REFERENCES:
- American Petroleum Institute. (2019). Standard 560: Fired Heat Exchangers for the Petroleum and Chemical Industry. API Publishing Services.
- National Fire Protection Association. (2020). NFPA 31: Standard for the Installation of Oil-Burning Equipment. National Fire Protection Association.
- International Organization for Standardization. (2021). ISO 13732-1: Ergonomics of the Thermal Environment — Methods for the Assessment of Human Exposure to Contact with Surfaces. ISO.
- Fluid Handling Institute. (2022). Hot Oil System Operation and Maintenance Best Practices. FHI Technical Report Series.
Xinxiang Huayuan Container Equipment Co., Ltd.
With abundant experience, we are one of the most reliable hot oil boiler manufacturers and suppliers in China. We warmly welcome you to buy durable hot oil boiler made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: No.2, South Road, Industrial Cluster Zone, Genghuang Township, Fengquan District, Xinxiang City, Henan Province
E-mail: cncd527@gmail.com
WebSite: https://www.huayuanequipment.com/
